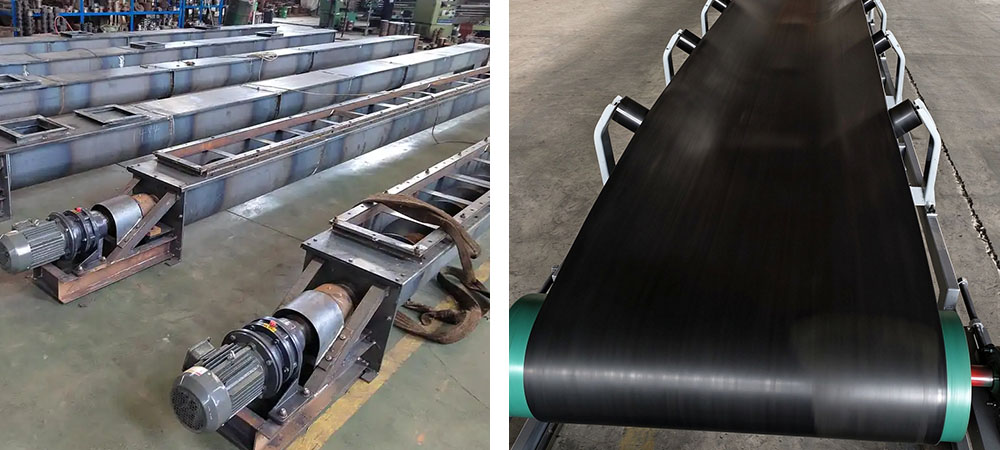
Quick Verdict: Screw Conveyor vs Belt Conveyor in Cement Industry
Choose a belt conveyor for long-distance bulk material transportation, especially for heavy, abrasive, high-temperature materials such as cement clinker and raw stone aggregate. It is the ideal solution for high-capacity, low-energy-consumption long-haul conveying in cement plants.
Core Differences Between Belt Conveyor and Screw Conveyor for Cement Plant
The following detailed comparison table covers all critical factors cement plant engineers care about, including conveying distance, material adaptability, dust tightness, inclination angle, energy consumption, and upfront & operational cost, helping you quickly screen suitable cement plant conveying equipment.
Comparison Factor | الحزام الناقل | ناقل لولبي |
نقل المسافة | Long-distance conveying, supporting hundreds of meters of continuous material transport; suitable for cross-plant and stockyard-to-kiln long-haul delivery | Short-distance conveying, with an economical effective length of under 30 meters; not applicable for long-distance bulk transfer |
Applicable Materials | Coarse-grained, abrasive, and high-temperature bulk materials, including hot cement clinker, limestone, gravel, and coarse raw aggregates | Fine, dry, free-flowing powdery materials, including finished cement powder, cement raw meal, fly ash, and mineral powder |
Enclosure & Dust Control | Open-type or partially covered structure; difficult to achieve full dust sealing, easy to produce dust pollution in dry working environments | Fully enclosed tubular structure, complete dust-tight performance; zero material leakage and dust emission, meeting environmental protection standards for cement production |
Maximum Incline Angle | Limited conveying inclination; large-angle conveying requires special customized anti-slip design, otherwise material slipping will occur | Supports steep incline and vertical small-height conveying, flexible installation angle, strong adaptability to complex plant layouts |
كفاءة الطاقة | Low energy consumption per ton of material; higher energy efficiency for long-distance and large-volume continuous conveying | Higher power consumption and energy cost; low efficiency for large-volume long-distance material transfer |
Cost Performance | High upfront installation and equipment cost, low long-term operation and maintenance cost, suitable for long-term large-scale production | Low initial investment cost, simple installation, but higher wear and maintenance cost in long-term operation with limited conveying range |
When to Use a Belt Conveyor in Cement Production
Belt conveyors are the mainstream bulk conveying equipment for large and medium-sized cement plants, widely used in the front-end raw material transportation and clinker conveying links. You should select a cement plant belt conveyor in the following scenarios:
- Long-distance bulk material transportation: When you need to transport materials between stockyards, raw material warehouses, rotary kilns, and finished product workshops spanning hundreds of meters, belt conveyors are the most stable and efficient choice.
- Handling abrasive and high-temperature materials: Hot cement clinker and coarse limestone aggregates have strong wear resistance and high residual temperature. Belt conveyors with heat-resistant rubber belts can effectively avoid rapid equipment wear, which is a fatal problem for screw conveyors.
- High-capacity continuous production: If your cement production line requires large-volume, uninterrupted material feeding, belt conveyors feature large conveying capacity and stable operation, reducing unit material energy consumption and improving overall production efficiency.
- Low long-term maintenance demand: Belt conveyor structures are simple and durable, with low failure rates and long service life, effectively reducing downtime and maintenance costs for cement production lines.
When to Use a Screw Conveyor in Cement Production
Screw conveyors, also known as spiral conveyors, are specialized powder conveying equipment tailored for fine materials in cement plants. They are irreplaceable in closed powder transfer links. It is recommended to choose a cement plant screw conveyor under the following working conditions:
- Short-distance fine powder conveying: Ideal for transferring cement powder, raw meal, and fly ash within 30 meters, such as material transmission between silos, grinding mills, and dust collectors.
- Dust-free and environmentally friendly conveying: The fully enclosed tubular structure completely avoids powder leakage and flying dust, perfectly meeting the strict environmental protection emission requirements of modern cement factories.
- Narrow space installation and feeding: Screw conveyors feature small footprint and flexible installation, suitable for narrow and compact equipment gaps where belt conveyors cannot be arranged, realizing precise feeding and discharging.
- Quantitative material feeding: The spiral rotation speed can be accurately adjusted to realize quantitative and uniform material supply, which is widely used in the feeding link of cement grinding systems.
Practical Application Combination in Real Cement Plants
In actual cement production line design and operation, screw conveyors and belt conveyors are complementary rather than competitive. Professional cement plant design schemes always adopt a combined conveying system to maximize production efficiency.
Generally, cement factories deploy heavy-duty belt conveyors for long-distance transportation of raw stone and hot clinker to undertake large-volume bulk material handling tasks. Meanwhile, compact screw conveyors, matched with air slides and دلو المصاعد, are used for short-distance closed conveying and quantitative feeding of various fine powders, ensuring dust-free production and precise material supply.
Frequently Asked Questions (FAQ) About Cement Plant Conveyors
We have sorted out the most frequently searched questions by cement plant purchasers and technicians to solve your daily equipment selection and operation doubts.
1. Which conveyor is best for cement powder transfer?
For short-distance, closed, dust-free cement powder conveying within 30 meters, a screw conveyor is the best choice due to its fully enclosed structure and no powder leakage. For long-distance centralized transportation of finished cement products, a customized belt conveyor with dust cover is more efficient and economical.
2. Can you use a screw conveyor to transport cement clinker?
It is not recommended. Cement clinker is high-temperature, hard, and highly abrasive. Long-term clinker conveying will cause severe wear of the screw blade and cylinder, leading to frequent equipment failure and high replacement costs. Belt conveyors are the standard equipment for clinker transportation in cement plants.
3. What is the maximum conveying distance of a cement plant screw conveyor?
The economical service distance of a standard screw conveyor for cement powder is within 30 meters. When the conveying distance exceeds 30 meters, the equipment power consumption increases sharply, and the failure rate of material blockage and blade damage rises. At this time, belt conveyors or bucket elevators are more cost-effective.
4. Which is more cost-effective for cement plant conveying: screw conveyor or belt conveyor?
For short-distance powder feeding scenarios, screw conveyors have lower upfront investment and higher cost performance. For long-distance, large-volume, and abrasive material conveying, belt conveyors have lower comprehensive operation costs and longer service life, making them more suitable for long-term cement production operation.
الأفكار النهائية
Selecting the right conveying equipment is crucial to improving production efficiency, reducing energy consumption, and meeting environmental protection standards for cement plants. To sum up, belt conveyors dominate long-distance, high-capacity, and abrasive material conveying, while screw conveyors are specialized in short-distance, dust-free fine powder transfer.
By matching the conveyor type with your material characteristics, conveying distance, plant space, and budget, you can avoid equipment mismatch, reduce maintenance costs, and optimize the overall operating efficiency of your cement production line.
 English
 Russian
 French
 Portuguese
 Arabic
 Spanish
 Japanese