Many cement‑plant operators encounter a frustrating issue with transportadores de tornillo for cement powder: conveying performance works well at startup, yet actual throughput gradually falls after continuous running. Sometimes raising screw rotational speed brings temporary improvement; on other occasions, higher speed does not lift tonnage proportionally.
Too often, technicians jump to conclusions by checking only motor power or simply specifying a larger‑diameter screw. However, screw conveyors are fundamentally volume‑based bulk material handling equipment, not tonnage‑driven machines. For fine cement powder, changes in bulk density, material aeration, feed stability, and internal material buildup can all alter the real volume of material displaced per screw revolution. This is one of the most common pain points when running a screw conveyor for cement silo discharge or conveying blended mineral powders.
01 Understand the Core Principle: Screw Conveyors Move Volume, Not Tons
When procuring equipment, project teams commonly specify target rates like “20 t/h” or “30 t/h”. Nevertheless, screw conveyor internal capacity is governed by volumetric flow, which is heavily dependent on material bulk density. This distinction is critical when you learn how to calculate cement screw conveyor capacity correctly.
From published KWS bulk‑material engineering data, ordinary Portland cement has a reference bulk density of ~94 lb/ft³ (~1506 kg/m³). By comparison, aerated Portland cement registers merely 60‑75 lb/ft³ (~961‑1201 kg/m³). Both material states recommend a 30 % trough fill factor in KWS datasheets.
This dataset illustrates a critical point: for identical cement powder, shifting material conditions significantly change mass within each unit volume. If your screw conveyor was sized for one bulk‑density figure, any variation of cement aeration on‑site will lower measured ton‑per‑hour output — even with unchanged screw rotating speed.
02 How Aerated Cement Powder Changes Conveying Behaviour
Cement is a typical fine powder. During silo discharge, pneumatic conveying, dust‑collector return feed and other process steps, air can become trapped within cement particles. The powder turns highly fluidized and loose, lowering mass per unit volume. Many operators ask can a screw conveyor handle aerated cement safely, and the short answer is yes — but you must account for its reduced bulk density.
Using the engineering figures quoted above: normal Portland cement sits around 1506 kg/m³, while aerated cement falls to 961‑1201 kg/m³. Assuming the effective displaced volume per screw revolution stays roughly constant, looser aerated powder delivers lower mass for the same swept volume.
Field symptom: the screw spins normally and material fills the housing, but your weighing system reports reduced hourly tonnage. When facing insufficient output on cement augers, do not only adjust speed — inspect the physical condition of powder entering the screw inlet.
03 Unstable Feeding Also Triggers Reduced Real‑World Throughput
There is a major gap between theoretical screw conveyor capacity and real‑world performance: consistent feed supply. KWS screw‑conveyor design methodology highlights that capacity tables are calculated for controlled, stable feeding conditions, with defined fill factor, screw diameter and operating RPM. Separate design rules apply for flood‑fed screw feeders whose inlet remains fully submerged by material. It is important to understand the difference between screw feeder and screw conveyor for cement before sizing your system.
This distinction matters greatly. When cement silos suffer material bridging, arching or erratic discharge, even a theoretically adequately sized screw cannot sustain its design fill level. If actual feed becomes intermittent, portions of screw flights run partially empty, cutting forward‑pushed material per revolution. Cement screw conveyor bridging issues are often misdiagnosed as a screw defect, while the root cause sits in the silo and discharge cone.
Lower throughput may therefore originate upstream at your cement silo and feeding interface, rather than within the screw conveyor itself.
04 Material Inside Housing Does Not Equal Effective Conveying Capacity
This is one of the most widespread misjudgements in powder‑handling troubleshooting. Opening inspection hatches and seeing powder filling the trough does no mean all material is travelling towards the discharge outlet at design velocity.
Should cement absorb moisture, form lumps, or adhere persistently to housing walls and central shaft, static material buildup occupies usable cross‑sectional area. This shrinks the effective flow area for continuously transported fresh powder. This phenomenon is also the main cause of cement powder slips in screw conveyor without visible blockage.
Static deposits frequently build up at feed sections, trough bottom, end‑plates and flange joints. Visually the housing appears full, yet far less new material advances per rotation.
When assessing real conveying performance, focus on the effective volume of actively transported material instead of total material trapped inside the casing. It also explains why housing geometry, dead‑zone elimination, sealing and maintainability deserve attention during equipment design.
05 Can You Simply Increase Screw Speed to Fix Low Output?
Raising rotational speed is operators’ go‑to quick fix. In theory — given unchanged screw diameter, flight pitch and stable fill factor — higher RPM increases theoretical volumetric throughput.
Unfortunately, these ideal conditions rarely persist on‑site. KWS engineering manuals note maximum tabulated speeds apply mainly for non‑abrasive, free‑flowing bulk solids. Most cement‑plant industrial installations require derated operating speeds.
If low throughput stems from poor silo feeding, aerated powder or internal buildup, speeding‑up the screw cannot resolve root upstream problems. Paradoxically, higher RPM can reduce fill per flight, so faster rotation fails to raise ton‑per‑hour proportionally.
06 Why Abrasion & Wear Must Be Considered for Cement Powder
Even though cement exists in powdered form, abrasion cannot be ignored. Both ordinary and aerated Portland cement are classified as Class II abrasive material in KWS bulk‑material characteristic tables. For abrasive bulk solids, engineers adopt conservative fill‑factor values and reinforced component design. Many users wonder what fill factor for cement powder screw conveyor is recommended; 25–30% is standard for abrasive cement, lower than free‑flowing non‑abrasive powders.
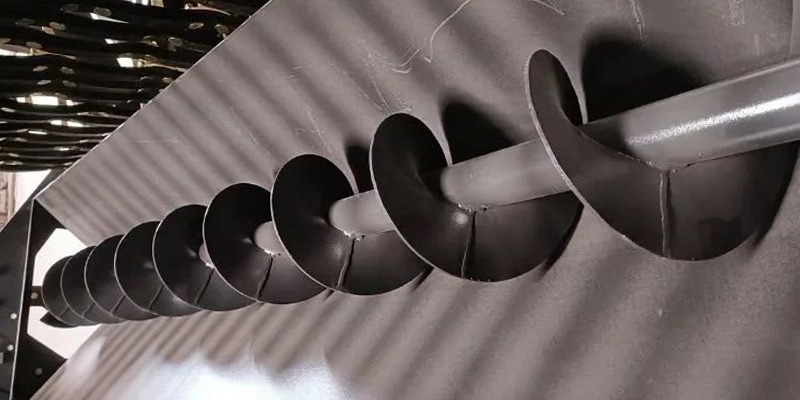
Over long‑term operation, outer edges of screw flights wear thin. This enlarges clearance between flight tips and the trough housing. Excessive clearance allows powder back‑flow and material slippage, weakening material propulsion per revolution. Screw conveyor flight wear causes low throughput gradually over months and years, rather than appearing as a sudden failure.
For ageing cement screw conveyors experiencing gradual capacity loss, inspect:
- Outer‑diameter wear of screw flights
- Trough housing abrasion
- Actual gap between flight tips and trough wall
07 Recommended On‑site Troubleshooting Sequence for Dropped Throughput
If your cement screw conveyor once hits design throughput but capacity gradually degrades, adopt this workflow: Material Condition → Feeding System → Internal Equipment Inspection → Operating Parameters. Avoid adjusting motor speed as your very‑first step.
- Check material status: Confirm if cement powder is heavily aerated, damp or lumpy. Compare real‑world bulk density with original design assumptions.
- Audit upstream feeding: Inspect cement silo for bridging / arching and fluctuating discharge. Verify continuous, stable material supply to screw inlet.
- Inspect equipment internals: Look for static buildup at feed zone, trough base and discharge area. Measure flight wear and actual flight‑to‑trough clearance.
- Review operating parameters: Validate real rotational speed, fill factor, conveying length and installation inclination.
Only after identifying the true bottleneck should you decide whether to modify rotating speed, rework silo‑feeding geometry, remove accumulated deposits or replace worn components.
Conclusión final
Falling tonnage output for cement‑powder screw conveyors is rarely caused by one single parameter shift. Bulk‑density drift changes mass‑per‑volume; powder aeration modifies flow properties; unstable silo feed lowers real fill factor; internal static buildup reduces usable conveying space; flight abrasion and enlarged clearances degrade material propulsion.
When you observe reduced throughput, do not immediately crank up motor RPM. Ask these critical questions first:
Preguntas frecuentes
Q1: What is the best fill factor for a cement powder screw conveyor?
A: For ordinary Portland cement and aerated cement, the industry standard recommendation is 30% fill factor or lower. Since cement is Class II abrasive, engineers often use 25–30% fill factor to reduce wear, backflow and powder slip. Higher fill factors are not recommended for cement, even if you want higher throughput, as abrasion risk and material backflow will increase.
Q2: Can a screw conveyor handle aerated cement from air slides or pneumatic conveying?
A: Yes, but you must re‑evaluate capacity based on the lower bulk density of aerated cement. Aerated cement occupies a larger volume per ton. A screw sized for normal cement bulk density will show reduced tonnage output when fed with aerated cement, even if volumetric flow stays the same. Many cement plants pair air slides with screw conveyors, so this condition is extremely common.
Q3: What is the difference between a screw feeder and a screw conveyor for cement service?
A: A screw feeder is flood‑fed; the inlet is fully covered by material and it meters discharge from a silo. A standard screw conveyor runs under controlled feed, with a defined fill factor. Mixing up these two design models is a frequent reason for unstable cement feed and low throughput.
Q4: Why does cement powder slip inside the screw instead of moving forward?
A: Slippage usually comes from two main factors: excessive clearance between flight tips and trough housing, or highly aerated, low‑density cement powder with very low inter‑particle friction. When slip occurs, the screw rotates, but the powder does not advance at the same rate.
Q5: How do I stop silo bridging and arching that starves my cement screw conveyor?
A: Silo bridging is a feeding‑side problem, not a screw fault. Common fixes include proper hopper slope design, silo aeration pads, vibrators, or flow‑aid devices. If the feed to the screw inlet is intermittent, no screw speed adjustment can maintain stable tonnage.
Q6: Is higher screw speed always better for cement powder conveying?
A: No. Higher speed raises volumetric capacity only when fill factor stays consistent. For abrasive cement, excessive speed accelerates flight and trough wear, creates more powder slip, and may reduce the actual fill per flight. KWS and most bulk material guides recommend conservative operating speeds for cement.
Q7: How often should I inspect screw flight wear on cement augers?
A: For continuous cement plant duty, schedule clearance and flight outer diameter inspection every 3–6 months. If you notice gradual throughput loss without changes in feed or powder condition, flight wear is the top suspect.
Q8: Can this screw conveyor design also work for fly ash, slag powder and mineral powder?
A: Yes. The same troubleshooting principles apply for fly ash, ground granulated blast furnace slag (GGBFS), limestone powder and other fine mineral powders. The key variable you must adjust is each material’s unique bulk density, abrasion class and flow behaviour. Darko supplies custom augers for these powder materials alongside cement.
Custom Screw Conveyor Solutions from Darko
If you are designing, retrofitting or sourcing non‑standard screw conveyors / augers for cement, mineral powder or fly‑ash handling, share your project parameters including:
- Material name & measured bulk density
- Target conveying throughput
- Conveying length and installation angle
- Feeding arrangement
- Existing equipment specifications or drawings
Darko’s engineering team conducts comprehensive analysis for screw diameter, flight pitch, operating speed, fill factor, central shaft and flight construction to deliver custom‑tailored bulk‑powder handling solutions for cement‑plant conditions.
 English
 Russian
 French
 Portuguese
 Arabic
 Spanish
 Japanese